Inquiry
Form loading...

Why Is the Right Tooling for Lathe Machines Important?

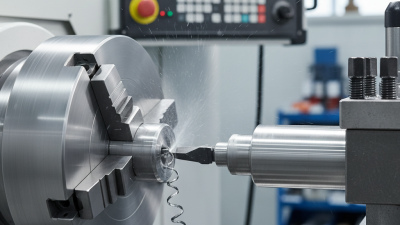
Why Is the Right Tooling for Lathe Machines Important? The answer begins at the cutting edge, where a small insert meets steel, aluminum, or titanium at high speed. Tooling For Lathe operations directly influences dimensional accuracy, surface finish, cycle time, and operator safety. A worn insert can leave a visible spiral on a shaft within seconds. It can also increase heat, vibration, and scrap.

Industry data supports this practical view. The Association for Manufacturing Technology’s U.S. Manufacturing Technology Orders reports consistently track strong demand for advanced machine tools and production equipment. These investments only deliver value when cutting tools match machine capability, material grade, and production volume. The CECIMO Economic and Statistical Reports also highlight automation, productivity, and skills as central pressures for European manufacturers. Proper tooling supports all three areas. It reduces manual correction and makes process results more repeatable.

Small choices matter. A rigid holder, suitable insert geometry, and correct coolant strategy can protect tolerances during long production runs. The International Organization for Standardization provides relevant guidance through standards such as ISO 13399 for cutting-tool data representation. That standard improves communication between tooling suppliers, software systems, and machinists. However, tooling decisions are not purely theoretical. Real workshops face interrupted cuts, uneven stock, limited budgets, and rushed changeovers. A laboratory-perfect recommendation may fail beside a noisy lathe. That is measurable.

For this reason, selecting the right tooling requires experience, verified supplier data, and controlled trial cuts. Manufacturers should compare tool life, chip control, finish, and total cost per component. The cheapest insert is rarely the lowest-cost choice. Good tooling turns machine capacity into reliable production.
Why Is the Right Tooling for Lathe Machines Important?

What Lathe Tooling Is and How It Supports Machining

Lathe tooling refers to the cutting tools and holders used to shape rotating workpieces. These tools remove material through turning, facing, threading, boring, and grooving operations. Each task requires a suitable cutting edge, clearance angle, and tool position. A small mismatch can create vibration, poor surface finish, or unnecessary tool wear.

The right tooling supports machining by controlling cutting forces and heat. For example, a rigid boring bar helps maintain accuracy inside a deep hole. A sharp turning tool can produce a cleaner shoulder on steel or aluminum. Tool material also matters, especially when cutting hard alloys or running at higher speeds. Experienced machinists check the workpiece material, diameter, tolerance, feed rate, and machine rigidity before choosing a setup.

Details at the tool tip matter. Even a tiny height error can leave a visible mark on the workpiece. Proper clamping reduces movement, while regular inspection helps detect chipped edges early. In real workshops, tool selection is not always perfect. A setting that works well today may perform poorly after material changes. I have seen operators blame the insert when the real issue was excessive runout or weak workholding. Small errors matter. Careful measurement, controlled trials, and documented adjustments make lathe tooling more reliable.
How to Match Cutting Tools with Lathe Materials and Operations

Why Is the Right Tooling for Lathe Machines Important?

Matching a cutting tool to the workpiece material improves surface quality, tool life, and machining control. Carbon steel usually responds well to carbide inserts with a stable cutting edge. Softer aluminum often needs a sharp, polished tool that reduces built-up edge. Stainless steel generates heat quickly, so a tougher grade and steady feed can prevent chipping.

The operation also changes the tool choice. Rough turning needs a strong insert with a suitable nose radius. Finishing passes benefit from a sharper edge and smaller cutting depth. Boring requires a rigid bar because vibration can leave repeating marks inside the hole. Threading demands the correct profile and a carefully controlled feed. Parting tools need accurate alignment and steady coolant flow.

Small details matter.

In practice, machinists should check the material certificate, tool geometry, spindle speed, and machine rigidity before cutting. Cutting charts provide a starting point, not a guarantee. I have seen a recommended speed fail when the workholding was weak. That mistake taught me to inspect the setup before blaming the insert. A clean toolholder, correct tool height, and measured runout often solve problems that seem more complicated. Operators should also watch chip shape, cutting sound, and surface color during the pass. These signs can reveal excessive heat or an unstable cut earlier than a final inspection. Sometimes, a slightly slower feed produces a better result, although it may reduce productivity. Reliable decisions come from recorded results, consistent measurements, and careful adjustment.

Key Factors in Selecting Accurate and Durable Lathe Tooling

Why Is the Right Tooling for Lathe Machines Important?

Key Factors in Selecting Accurate and Durable Lathe Tooling

Choosing accurate and durable lathe tooling begins with the material being cut. Aluminum, stainless steel, and hardened steel each create different cutting demands. Tool geometry must match the job, not just the machine. Rake angle, clearance, and nose radius influence cutting force, surface finish, and vibration. A small mismatch can leave chatter marks on a shaft.

Experienced machinists also check rigidity before selecting a tool. A long, thin boring bar may deflect inside a deep hole. A larger shank often provides better support. Tool overhang should remain as short as practical. Coolant delivery matters too, especially during continuous production. Heat can soften an edge and shorten tool life quickly. These details are easy to overlook.

Durability depends on more than tool material. Cutting speed, feed rate, setup quality, and chip control all matter. Carbide may perform well in stable conditions, while high-speed steel can offer useful toughness for certain operations. I have seen a costly tool fail because the workholding was slightly loose. The catalog choice was not the real problem. Inspection should include edge wear, dimensional drift, and surface changes during the run. Tool life records can reveal patterns, but they are not perfect. Operators still need judgment. Sometimes, a slower cut produces better accuracy and lower waste.

Why Is the Right Tooling for Lathe Machines Important?

Typical cutting-speed ranges for turning steel vary significantly by tool material. Selecting accurate and durable tooling helps achieve stable machining, longer tool life, and higher productivity.

Representative industrial ranges in meters per minute for steel turning. Actual values depend on workpiece hardness, tool geometry, depth of cut, feed rate, coolant, and machine rigidity.

How Proper Tooling Improves Lathe Safety, Efficiency, and Quality

Why Is the Right Tooling for Lathe Machines Important?

Proper tooling directly affects lathe safety, machining efficiency, and finished-part quality. A correctly selected cutting tool sits firmly in the holder and reduces vibration during rotation. Stable tooling helps prevent unexpected tool movement, damaged workpieces, and sharp chip hazards. Operators should check tool condition, clamping force, and clearance before cutting. Small checks matter.

Tool geometry must match the material, cutting speed, feed rate, and turning operation. A suitable insert can produce cleaner surfaces and more predictable dimensions. Good chip control also keeps the work area clearer and reduces interruptions. In daily production, this means fewer tool changes and more consistent cycle times. However, faster cutting is not always better. Excessive speed can create heat, shorten tool life, and affect dimensional accuracy.

Quality depends on more than the tool itself. Proper alignment, accurate setup, coolant control, and regular inspection all contribute to reliable results. Even experienced operators can overlook gradual wear, especially during long production runs. That is a real weakness. Measuring the first part and checking critical dimensions during production can expose problems early. A perfect setup is rare, so teams should record useful observations and adjust methods when evidence supports a change. This practical discipline improves safety, efficiency, and repeatable quality over time.

Why Is the Right Tooling for Lathe Machines Important? - How Proper Tooling Improves Lathe Safety, Efficiency, and Quality

Tooling Dimension Practical Guideline or Typical Value Safety Contribution Efficiency Contribution Quality Contribution Relative Impact
(1–5)
Tool Overhang Keep external turning-tool overhang as short as practical; for boring, a steel bar is commonly limited to about 4× diameter, while a carbide bar may reach approximately 6–7× diameter under suitable conditions. Reduces vibration, tool deflection, and the risk of an unstable cut. Allows more consistent cutting parameters and reduces rework caused by chatter. Improves dimensional stability and surface finish, especially in internal turning. 5
Toolholder and Workholding Runout Use a clean, rigid setup and verify runout with a dial indicator. A practical precision target for finish operations is often around 0.01 mm or less, depending on the machine and process. Limits uneven loading, insert breakage, and unexpected workpiece movement. Improves tool life by preventing one cutting edge from carrying excessive load. Supports repeatable diameter, concentricity, and wall-thickness results. 5
Insert Nose Radius Common turning nose radii include 0.4 mm, 0.8 mm, and 1.2 mm. Smaller radii suit light cuts and weak setups; larger radii can improve finish when the machine and workpiece are rigid. Matching the radius to setup rigidity helps prevent chatter and sudden insert failure. Larger radii can support higher feed rates when cutting conditions are stable. A properly selected radius improves feed marks, edge strength, and profile accuracy. 4
Feed Rate Relative to Nose Radius For general finishing, a useful starting relationship is feed per revolution at approximately 0.25–0.50× the nose-radius value, then adjust according to material, insert geometry, and required finish. Prevents excessive cutting forces that can cause workpiece movement or insert damage. Balances cycle time against tool wear and surface-finish requirements. Helps produce a predictable surface pattern and reduces the risk of tearing. 4
Clearance and Lead Angles Many general-purpose turning tools use a relief angle in the approximate range of 5–7°. Lead angle and rake should be selected according to material, cut direction, and available rigidity. Provides clearance between the tool flank and workpiece, reducing rubbing and heat generation. Reduces cutting resistance and can improve chip control when correctly matched to the operation. Minimizes rubbing marks, dimensional drift, and poor edge definition. 4
Insert Grade and Geometry Use a tougher geometry for interrupted cuts or unstable setups and a sharper geometry for light finishing cuts. Select carbide grade and coating according to the workpiece material and cutting temperature. Reduces the likelihood of edge chipping and catastrophic insert failure. Improves usable tool life and reduces insert changes during production. Maintains a more consistent cutting edge, supporting repeatable tolerances. 5
Chipbreaker Selection Choose a chipbreaker that matches the planned feed and depth of cut rather than using one geometry for every operation. Helps break long, hazardous chips and reduces the need for manual chip removal. Supports continuous machining with fewer interruptions and less downtime. Reduces chip recutting, surface scratching, and unpredictable tool loading. 5
Coolant Delivery Direct coolant or cutting fluid toward the cutting zone when the workpiece material and tool system require it. Keep flow consistent and avoid obstructing chip evacuation. Controls heat and helps prevent chips from accumulating around the cutting area. Can improve tool life and reduce cycle interruptions caused by overheating. Supports stable dimensions and a more consistent surface finish. 4
Tool Center Height Set the tool tip accurately on the spindle centerline; verify the setting after tool changes, especially for threading, grooving, and form tools. Prevents abnormal cutting forces and reduces the chance of tool interference. Improves predictability during setup and reduces adjustment time. Supports correct thread form, diameter control, and profile accuracy. 5
Tool Inspection and Replacement Inspect cutting edges for chipping, built-up edge, flank wear, and thermal damage. Replace or index the insert before wear causes dimensional drift. Reduces the risk of sudden breakage and flying fragments. Prevents extended production runs with declining cutting performance. Maintains consistent tolerances and surface quality from part to part. 5

Note: The numerical values are common starting guidelines for general turning practice, not universal limits. Final tooling choices and cutting parameters should be validated against the workpiece material, machine rigidity, spindle power, insert manufacturer data, workholding method, and required tolerance.

How to Maintain and Replace Tools for Reliable Lathe Performance

Reliable lathe performance depends on disciplined tool maintenance, not only on machine power. Inspect the cutting tool before each shift. Look for chipped edges, built-up material, loose holders, and unusual discoloration. A sharp edge should meet the workpiece cleanly. Dull tools often leave burn marks, poor finishes, and changing dimensions.

Clean the holder and tool pocket with a soft brush and approved cleaner. Even a thin chip can affect tool alignment. Check clamping bolts with the correct torque method, rather than guessing by hand. Confirm that the tool sits at the proper center height. Record tool life, cutting material, workpiece type, and operating conditions. These notes help technicians identify repeated failures. I once replaced a tool too late because its poor finish seemed like a setup problem. That mistake cost time.

Replace a tool when wear reaches the permitted limit, not only after visible breakage. Follow the tool maker’s specifications and the machine’s maintenance procedures. Use protective equipment during handling, and stop the machine before making adjustments. After replacement, verify the insert seating and run a controlled test cut. Measure the diameter and surface finish with calibrated instruments. Listen carefully, too. A sudden change in vibration or cutting sound deserves inspection. Perfect records are unrealistic, but careless records are worse.